Ask a print buyer about dtg vs screen printing and the conversation usually turns to price per piece or which one looks better. Both questions come too late. Long before cost or finish enters the picture, each method has already decided what your artwork is allowed to be: how many colors it may contain, how fine its lines may run, how its gradients must be built, and what happens when the shirt underneath is black. Draw first and choose the method afterward, and the file you made is often unprintable as drawn. This article works the problem in the productive direction: what each method demands, which four decisions pick the method for you, which artwork fails both, and how to check a file against the method chosen.
Artwork Constraints Run Backward from the Method
A print file is not a picture. It is an instruction set for a specific machine, and the machine's physics decide which instructions exist. Screen printing pushes ink through a patterned mesh, one stencil per color. DTG jets water-based ink directly into the fabric, like a desktop printer into paper, and fixes it with heat. Two machines, two physics, two completely different sets of legal instructions.
Designers are trained to work forward from an image in the head: subject, palette, composition. Production works backward from the machine: what the press can lay down defines what the file may contain. When the two directions meet late, the file loses, because it quietly encoded assumptions — continuous tones, unlimited colors, hairlines anywhere, any garment color — that the chosen machine cannot honor.
None of the constraints below is a matter of taste or shop preference. Each is derived: once you picture the machine, the artwork rules stop being opinions and start being geometry, chemistry, and cost structure.
Screen Printing Thinks in Separations
The screen printing press is, at heart, a separation machine. Every color in the final print is one stencil, one screen, one pass of a squeegee. The file that feeds it is not one image but a stack of flat color layers, and every constraint a screen printer hands you follows from that architecture.
The first consequence is spot color thinking. Artwork must decompose cleanly into a small number of solid color layers. Flat illustration and bold shapes separate beautifully; soft airbrush blends and photographs do not, because there is no clean way to slice a continuous tone into discrete stencils.
The second consequence is that color count is a budget line, not a palette preference. Each additional color means another screen to expose, register on press, and wash out afterward. The ceiling is set by the shop's press capacity and per-screen setup pricing, and it varies from printer to printer — the right source for the number is your printer's spec sheet.
The third consequence is that gradients exist only as halftones. A screen cannot hold a fade, so it fakes one with dots: larger dots where the tone is dark, smaller dots where it is light, fabric showing through the gaps. The result is a legitimate printed texture, but it is a texture — a photographic gradient rendered this way becomes a different image, and dots finer than the mesh can hold drop out.
The fourth consequence is a floor under fine detail. Mesh and ink viscosity set a minimum below which lines plug the screen or vanish on the fabric. Hairlines that survive happily in a vector file may not survive the mesh.
The fifth consequence concerns dark garments. Bright ink cannot overpower a dark shirt, so the press first lays down a white underbase and prints the colors on top of it. The underbase is one more screen and one more layer to plan for: colors behave differently over white than over cloth, and the underbase's shape is itself a design decision.
Screen-ready artwork, then, is layered spot color art with a counted palette, deliberate line weights, and tones rebuilt as dots on purpose. Not a style — the file format of the machine.
DTG Thinks in Pixels
DTG is a different machine with a different file format. Print heads jet water-based ink straight into the fabric, so the file it wants is a raster image — pixels at final print size. The constraint set flips almost completely.
The freedom is real. Full color adds no per-color charge, because there are no screens to multiply. Photographic detail, soft shadows, and true continuous gradients all print as drawn. Where screen printing charges for every color and taxes every blend, DTG treats a sunset and a logo as the same job.
The first boundary is pixel discipline. The print can only carry detail the file actually contains, so a web-resolution image enlarged to chest size prints soft, and upscaling invents detail that was never there.
The second boundary is gamut. Water-based inks reproduce a wide but finite range of color. Fluorescent and neon tones sit outside it, and some specific spot colors — including brand colors defined as swatch values — cannot be matched exactly. A design that depends on an exact fluorescent hit is a design DTG cannot honor.
The third boundary is the dark-garment problem, and here it is DTG's turn to pay for white. Dark shirts receive a pretreatment and a jetted white underbase before the color pass. That underbase is an ink film with physical presence: the printed area feels firmer and smoother than the bare shirt, soft-edged artwork can show a faint outline where the underbase ends, and isolated hairlines over dark fabric may break or gain a halo. Large solid coverage compounds this — a dense rectangle on a dark tee can feel like a patch.
DTG-ready artwork is high-resolution raster art with rich tones, no out-of-gamut dependencies, and edges designed with the underbase in mind.
The Four Decisions That Pick the Method for You
A print method comparison sounds like a judgment call until you lay out the deciding facts. Four of them do nearly all the work, and all four are knowable before anyone draws anything:
Decision | Leans toward screen printing | Leans toward DTG |
Order length | Long runs of one design, where per-screen setup spreads thin | One-offs, short runs, and print-on-demand, where there is no setup to spread |
Color count | A small, countable palette of flat spot colors | Full color, photography, and gradients at no per-color cost |
Garment color | Bold opaque spot colors on darks, with an underbase planned as a layer | Light garments are simplest; darks print well but gain underbase hand and edges |
Fabric material | Cotton and blends, with specialty inks covering synthetics | High-cotton garments; water-based inks bond poorly to many synthetics |
None of these rows is a preference. The order-length row is arithmetic: screen printing buys setup once per color and amortizes it across the run, while DTG's cost per piece stays nearly flat. The fabric row is chemistry: water-based inks bond willingly to cotton and reluctantly to polyester, while plastisol screen inks sit on almost anything. Take your four answers to your printer's spec sheet and the method usually names itself.
Artwork That Fits Neither Method
The most expensive files fail both machines, and they share a root cause: their properties were set by aesthetics alone, so they carry assumptions no chosen method ever ratified.
The web-resolution collage is the universal failure. Screen separation turns its compressed edges into ragged color layers; DTG prints its blur faithfully at chest size. Neither machine can recover detail the file never had.
The photographic fade on a dark garment is the double bind. Sent to screen, its smooth gradient becomes a halftone texture over an underbase — a different image. Sent to DTG, it prints beautifully but sits on a white film whose edge and hand feel were never intended. Both outputs are technically successful and aesthetically wrong.
The neon brand palette fails in opposite directions on each press. DTG cannot reach fluorescent tones at all; screen printing reaches them with specialty inks, but only as planned spot colors, so the palette must be rebuilt as separations first. Handing a fluorescent photographic file to either machine as-is guarantees a miss.
Hairline linework with soft anti-aliased edges on dark fabric rounds out the list: below the mesh floor on one machine, haloed by the underbase on the other, and avoidable at the drawing stage in both cases.
The Right Order: Method First, Then Drawing
The fix is sequencing, not skill. Choose the method before the artwork exists and the constraints stop being surprises:
• Fix the order length and sales model first, because a stocked run and a print-on-demand listing point at different machines.
• Fix the garment color and fabric, because dark grounds and synthetics carry method-specific costs.
• Count the colors the design honestly needs, because that number is free for one method and priced per unit for the other.
• Read the method off those three answers, using your printer's spec sheet where economics decides.
• Draw inside the chosen method's constraints, with its file format as the brief.
The design decisions you already know still happen — subject, composition, palette, the whole layer of judgment described in the decisions that come before drawing. They simply happen inside the fence now, because the method decision sits one step earlier: it governs what the file may physically contain rather than what the picture says.
Run the chain forward and it is short: run length, garment, and palette select the method; the method dictates the file spec; the file spec frames the drawing. Run it backward and each stage has to be redone in the next stage's language.
Checking Artwork Against the Chosen Method
Acceptance means checking the file against the machine, not against taste. The checklist forks by method:
Check | Screen printing file | DTG file |
Structure | Separated spot layers, one per color, registered | Single raster at final print size |
Color definition | Spot values agreed with the printer | Full-color file with out-of-gamut tones flagged |
Finest element | Above the shop's line and halftone dot floor | Real pixels, never upscaled; hairlines tested on the intended garment color |
Dark-garment plan | Underbase drawn as an intentional layer | Underbase areas known; edges and hand feel accepted |
Placement | Size and position confirmed on a garment mock | Same |
Two rows catch most of the damage in practice: the finest-element row, because detail failures are invisible on a monitor and permanent on fabric; and the placement row, because a file can pass every technical check and still fail as a print — scale and position judged on an artboard are guesses about a chest.
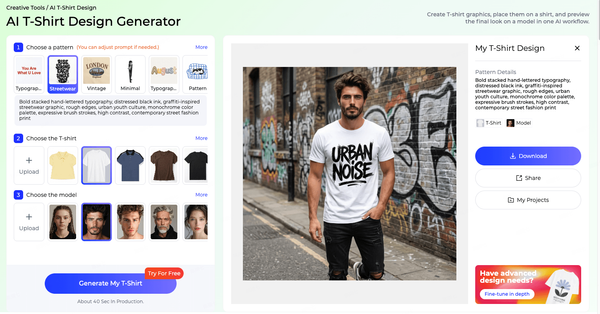
That last check is the one most workflows skip. Mapping the finished file onto a garment image at final print size turns placement and proportion into something checkable before sampling, and the placement print tool on Style3D AI — which applies a finished print to a garment image — exists for exactly this step. Whatever tool you use, verify against the garment rather than the flat artwork: the artboard and the file agree with each other by construction, so comparing them confirms nothing.
FAQ
Does gradient-heavy artwork always have to go DTG?
No. Screen printing reproduces gradients as halftones, and the visible dot texture is a legitimate look in its own right. The dividing line is photographic smoothness: if a visible dot structure would ruin the design, it belongs on DTG; if printed-dot character is acceptable or wanted, screen printing is still in play.
Who sets the color-count ceiling for screen printing?
Your printer's press and pricing structure set it. Every color is one more screen to expose, register, and wash, so the ceiling is economic and mechanical, not aesthetic. Ask the shop for its maximum color count and per-color pricing before you finalize a palette.
Why does DTG on a dark shirt feel different from the same print on a light one?
Dark garments get a pretreatment and a white underbase before the color pass, so more ink sits on the fabric surface. That extra film is what you feel as a firmer patch, and its edge is why soft artwork boundaries can look faintly outlined on dark fabric.
Which method should I use for a single piece or a tiny test run?
DTG. Screen printing's setup is charged per color per design and only disappears when spread across a real run; DTG has no comparable setup, so one-offs and samples are its home ground.
Can one artwork serve both methods?
Yes, if you keep a layered master and export two production files from it: separated spot layers for screen printing, a flattened high-resolution raster for DTG. What fails is a single flattened web-size file, which holds neither the layers screen printing needs nor the detail DTG needs.
Do vector files pair with screen printing and raster files with DTG?
Broadly, yes. Vector art separates cleanly into spot layers and scales without loss, which is what screen printing wants. DTG prints pixels regardless, so supply a high-resolution raster at final print size and the conversion loses nothing.
Where this leaves you
Artwork specs are the print method wearing a disguise. Screen printing turns art into separations and charges for every color, dot, and layer; DTG turns art into pixels and charges for resolution, gamut misses, and the white film under dark shirts. Four decisions — order length, color count, garment color, fabric — pick the method before any sketch begins, and the method then writes the brief the drawing must obey. Decide the method first, then draw. The reverse order does not save design time; it converts it into rework.
Check the Print on the Garment Before You Commit
Take the artwork you have already specced against its method and run the last check on the garment itself: placement, scale, and proportion on a real chest rather than an artboard. Map the finished file onto a garment image at final print size, confirm the print sits where the design intends, and only then release it for sampling or production. A file that passed every technical check can still miss as a placed print, and the garment preview is where that miss shows up. One preview now costs less than one reprint later.
Written by